Welding
Rochester Welding specializes in TIG, MIG, and robotic welding produced by seasoned professional welders. We have a vast library of qualified welding procedure specifications that includes various grades of stainless steel, carbon steel, aluminum and steel armor plate using both semi-automatic and manual welding processes.
UPSTREAM core competencies:
- Drawing review and aid in bidding prospective projects with PMs and Estimating Dept.
- Make use of APQP and manufacturability & constructability reviews
- Involved in related manufacturing and processing team discussions
- Collective fixture conception, collaboration, and team review with Design Eng. Dept.
- Acquire, obtain, and implement proper welding equipment and best practices in effort to obtain code-level welding quality in a highly efficient manner.
- AWS Members, extensive latest edition resource Library maintained.
WELDING PROCESSES employed:
-
MIG welding – (GMAW-S, GMAW-P, GMAW)
-
TIG welding – (GTAW)
-
MIG-Aluminum – (push-pull GMAW-P, GMAW-Spray)
-
Robotic MIG welding – (Automatic GMAW-S, GMAW-P, and FCAW-GM)
-
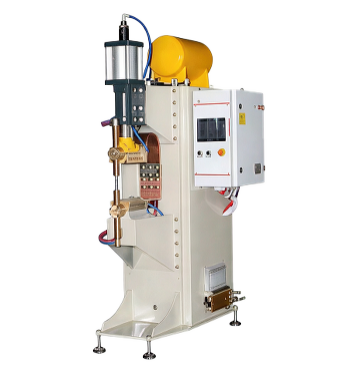
Resistance Spot/Projection Welding – RSW, PW
-
Flux Cored Arc Welding – FCAW-GM
-
Preheating and Interpass Temperature control
BASE METALS used (typical and “standards”):
Armor - 12560, 46100, and Domex Alloys
Carbon Steels - A36, A500, A513, A1011HR, A100CR, C1020
HSLA (High Strength Low Alloy) Steels - A572 Grade 50, A588, A656
HTLA (Heat Treatable Loy Alloy) Steels - A514 Grade B & H, A519 Grades 4130, & 4140
Stainless Steels and Nickel alloys - 304/304L, 316/316L, 321, Hastelloy X
Aluminum; Non Heat Treatable and Heat Treatable - 3003, 5052, 5083, 5086, 6061, and 6063
Expanded Metal - Flattened and Standard; Steel, SS, Al
FILLER METAL usage:
ER80/90S-D2, ER70S-6, and E100/110S
E70C, and E90C-D2
ER308L, R309L, R347, RNiCrMo-2
E308LT1-4
ER5356, E5183, and ER4043
SHIELDING GASES utilized:
90/10 (Ar+CO2) 95/5 (Ar+O2) 100% Ar (Argon)
75/25 (Ar+He) 75/25 (He+Ar) 75/25 (Ar+CO2)
95/5 (Ar+CO2) 98/2 & 95/7.5/2.5 100% He (Helium)
WELDING QMS (Quality Management System)
- In-house qualification to AWS (American Welding Society) D1, B codes, and MIL-STDs:
D1.1-Steel
TACOM Ground Combat Vehicle Welding Code-Steel
D1.2-Aluminum
D1.3-Sheet Steel
D1.6-Stainless
B2.1
D17.1-Aerospace
PQRs
(Procedure Qualification Records)
- Development
- Macroetch/macrograph
- Bend Tests
- Brinell
- RT/UT (outsourced)
- Tensile tests (pulls outsourced)
- Write-up
WPSs
(Welding Procedure Specifications)
- Write-up
- Weld Information Boards
- WPS matrices
- Continual training
WPQRs
(Welder Performance Qualification Records)
-
- Training
- Testing
- Certification
- Welder Continuity Logs and Matrices
- Welder Wallet Cards
- RT (outsourced on occasion)
- Macroetch/macrograph
- Bend Tests (performed internally; preferred over RT)
WELDING INSPECTION
- CWI two (2) Certified Welding Inspectors and one (1) CAWI oversight before, during, and after welding
- Filler Metal and Shielding gas CoCs, official reports, PPAP packages, Weld Maps.
Process Monitoring
- Use of calibrated Fluke 275 Amp-Voltmeter to verify adherence to WPS amperage, voltage, and Preheat & both min. & max. Interpass temperature essential variable ranges.
- GTFM (calibrated Gas Turbine Flow Meter), shielding gas flow verification.
Destructive Testing by way of
- Cut & Etch; -macroetch and macrograph capabilities for Carbon/Alloy Steel, Stainless, and Aluminum.
- Pry & peel and RSW button/nugget testing
- Torsion/Torque testing for projection weld nuts and studs
- Push-out testing for projection welded nuts and studs
NDE; 3rd Party ASNT Level II RT, PT, UT, MT services on call (Lab or Call out
WELDING OPERATIONS
- Job kitting; components and details for weldments are kitted with job traveler and drawings
- Welders, Welding Engineer, and CWI discuss (line-up) work before fabrication begins
- Certified WPQRs in 2G for plate, and 2G, 5G, & 6G for tube and pipe for all RWCI typical base metals.
WELDING EQUIPMENT
GMAW
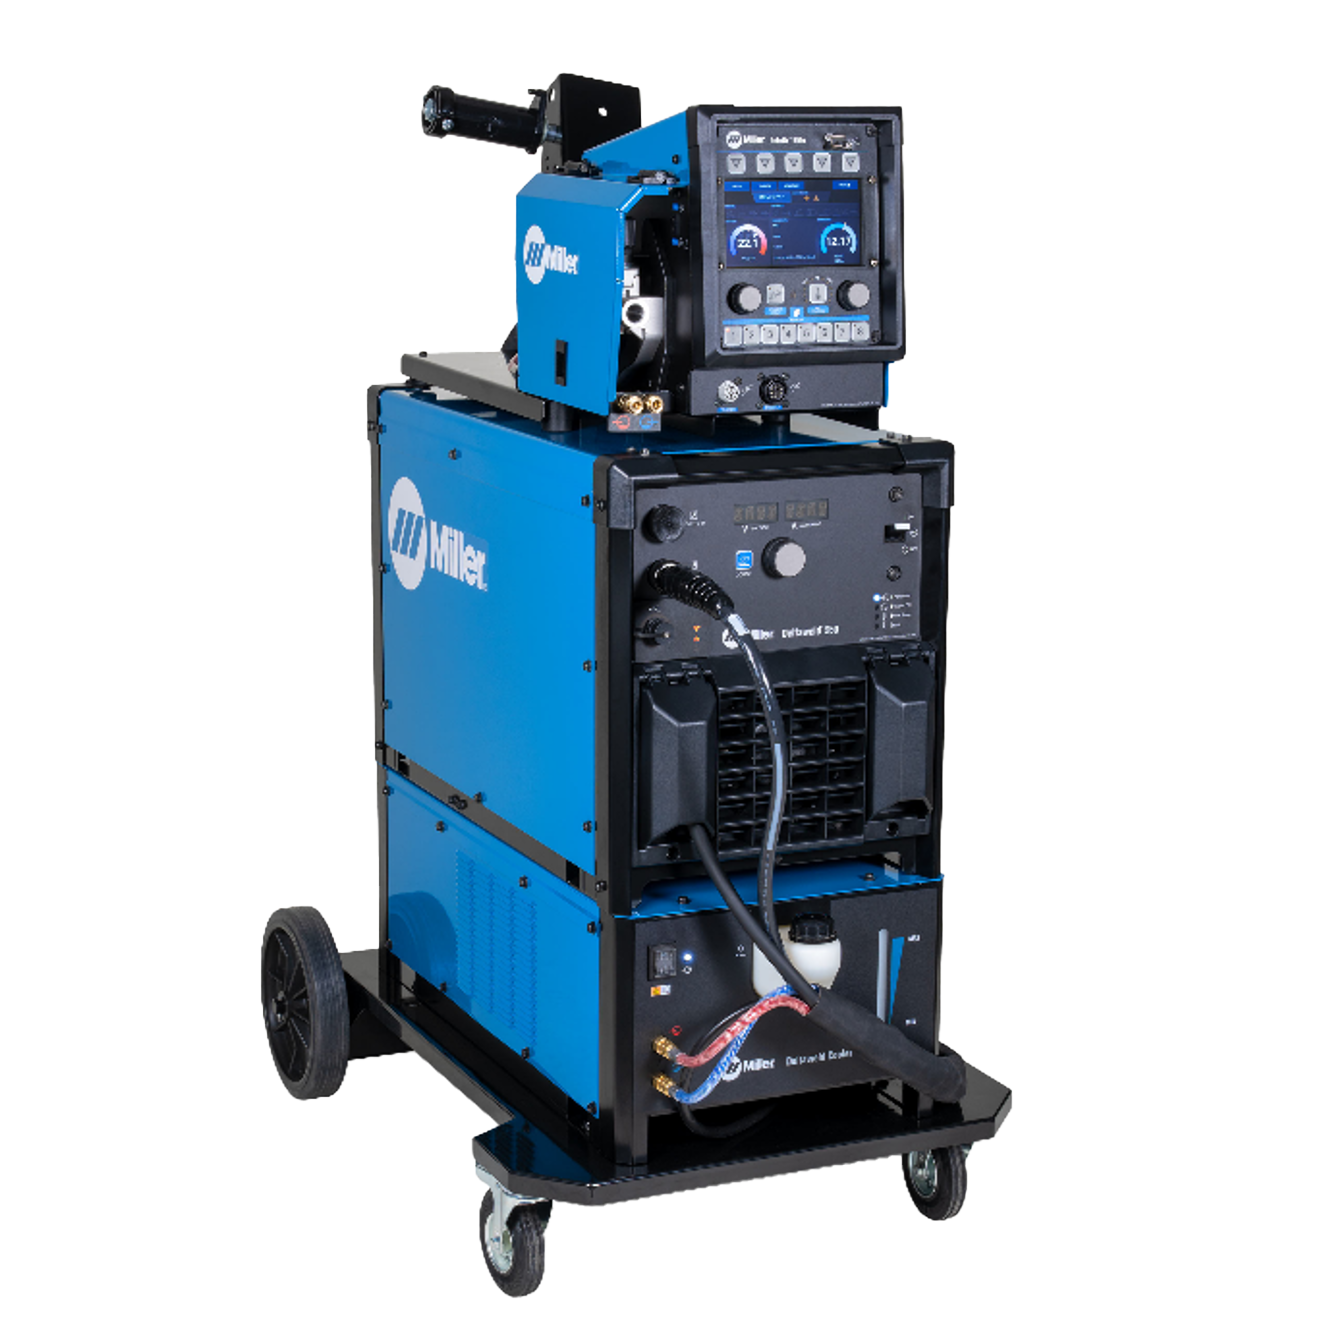
- 9 – Miller DeltaWeld 350 Dual Feed
- 2 – Lincoln PowerWave 455M
- 1 – Miller XR AlumaFeed
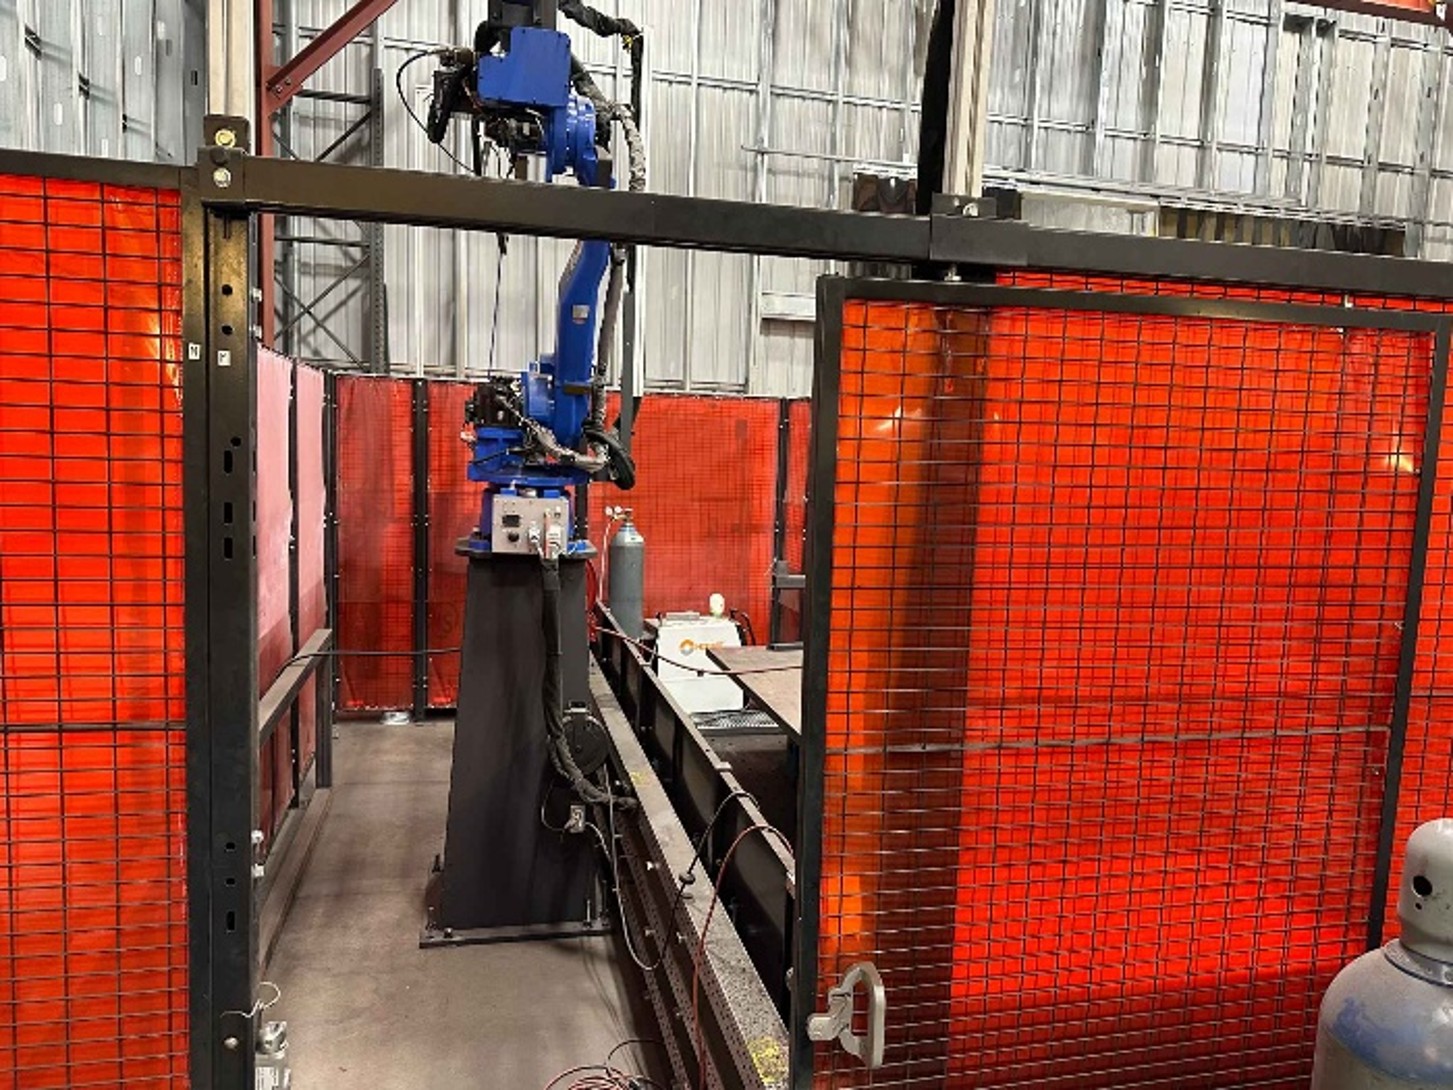
- 1 – Yaskawa Motoman powered by Lincoln Robotic Welder
GTAW
- 1 – Miller Dynasty 280
- 3 – Miller Dynasty 350
- 1 – Lincoln Precision TIG 375
- 1 – Lincoln Aspect 375
- 1 – Miller Dynasty 400
RSW
- 1 – Spot Weld Inc. Press Rite spot welder w/ WT6000 MFDC Welding Control